1. Fault Overview & Industrial Operating Symptoms
The Allen-Bradley PowerFlex 755 variable frequency drive (VFD) is a cornerstone of heavy continuous industrial automation, driving critical induction and permanent magnet motors across automotive, packaging, water treatment, and manufacturing facilities worldwide. However, when a PowerFlex 755 drive trips with F0002 (Overcurrent Fault), production halts immediately. This fault indicates that the drive's internal hardware current sensing circuit detected an instantaneous output current exceeding the hardware trip threshold (typically 200% to 250% of rated drive current).
In plant environments across Virginia and the Mid-Atlantic, facility technicians frequently attempt repeated fault resets or auto-tune cycles without resolving the underlying issue. While an F0002 fault can occasionally stem from external mechanical jams or shorted motor leads, intermittent F0002 trips during steady-state operation or immediate fault trips upon command run signal are classic indicators of severe internal hardware degradation within the VFD power stage.
2. Root Cause Analysis: Thermal Stress & Gate Optocoupler Degradation
Component-level root cause investigation by the Apex Industrial Control diagnostic team reveals three primary failure vectors responsible for persistent PowerFlex 755 F0002 faults:
- IGBT Module Thermal Fatigue & Bond Wire Drift: Under continuous high ambient temperatures and heavy torque cycles, internal Insulated Gate Bipolar Transistor (IGBT) silicon dies undergo extreme thermal expansion and contraction. Over time, internal aluminum bond wires suffer from micro-fractures, elevating collector-emitter saturation voltage (VCE(sat)) and causing localized thermal hot spots.
- Optocoupler Propagation Delay Degradation: High-speed optical isolation ICs (such as HCPL-316J or ACPL-332J series gate drivers) transfer pulse-width modulation (PWM) signals from the main control board to the high-voltage inverter stage. Operating over thousands of thermal hours degrades LED output intensity inside the optocoupler, delaying turn-on/turn-off switching times and creating shoot-through cross-conduction risks.
- Current Sensing Shunt & Amplifier Drift: The drive's LEM current transducers and precision current-sense shunt resistors can shift in resistance due to electrical surges or solder joint oxidation, sending false high-current voltage spikes to the control processor DSP.
3. Component Diagnostic Methodology & Waveform Isolation
At the Apex Industrial Control bench laboratory in Chantilly, VA, diagnosing a PowerFlex 755 F0002 fault begins with strict un-powered cold resistance tests followed by high-voltage dynamic signal profiling. Technicians inspect internal power rails to prevent secondary catastrophic board damage before applying main line voltage:
Apex Industrial Control Bench Diagnostic Protocol for PowerFlex 755
- Static Diode Bridge Test: Measure forward/reverse bias voltage drops between output phases (U, V, W) and DC bus (+ / -) terminals to identify shorted or leaky free-wheeling diodes.
- Desaturation Circuit Verification: Test gate-driver desaturation protection diodes and clamp circuits designed to sense IGBT saturation fault conditions.
- Oscilloscope Gate Waveform Analysis: Utilizing 4-channel 200MHz digital storage oscilloscopes with high-voltage differential probes, engineers inspect PWM gate drive signals for overshoot, ringing, asymmetric rise/fall times, or negative turn-off bias breakdown.
4. Micro-Soldering Rework & Component Replacement Protocol
Replacing the entire drive assembly is rarely necessary when precision component-level rework is available. The Apex Industrial Control component rework process replaces degraded active components with OEM-grade or higher thermal specification components:
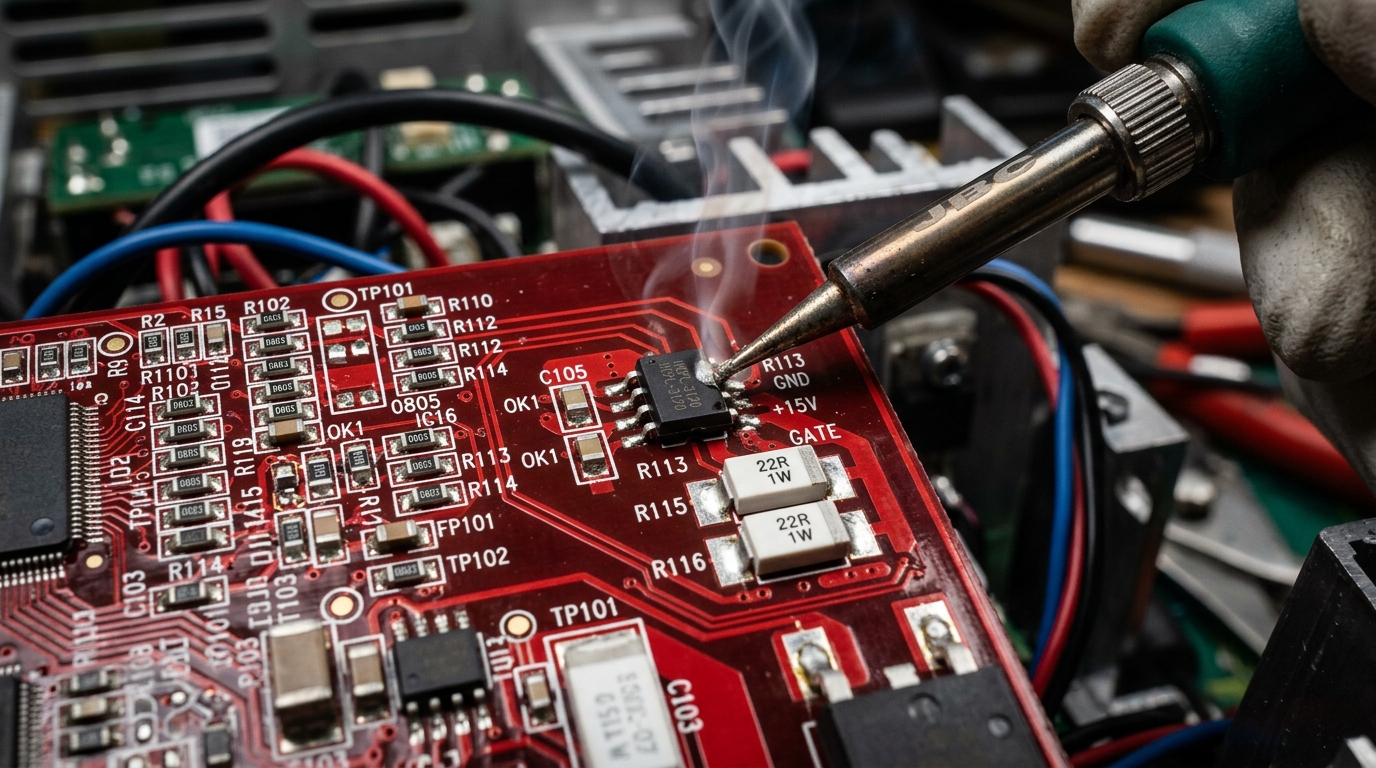
Using ESD-safe hot-air desoldering stations and high-magnification stereo microscopes, our bench technicians replace all six high-speed gate driver optocoupler ICs, gate resistors, and desaturation sense diodes. Degraded IGBT modules are removed, heatsink mating surfaces are precision-cleaned to remove dried thermal compound, and premium thermal grease with ultra-low thermal impedance is applied. Following component installation, multi-layer printed circuit boards undergo ultrasonic cleaning and receive a fresh application of military-grade polyurethane conformal coating to protect against industrial contaminants, humidity, and chemical vapors.
5. 460V Dynamometer Full-Load Validation & Thermal Stressing
Static bench testing alone cannot guarantee that an F0002 fault won't reappear when the drive is subjected to severe operating torque in an active manufacturing facility. Every PowerFlex 755 drive rebuilt at Apex Industrial Control must pass rigorous closed-loop load testing on our dedicated 460V dynamometer test stand.
Our automated load validation protocol at Apex Industrial Control subjects the repaired VFD to 100% rated motor current, rapid step-acceleration ramps, full-torque low-speed holding, and rapid regenerative deceleration cycles over an extended thermal saturation period. Infrared thermal imaging cameras monitor IGBT module surface temperatures and gate driver board heat distribution in real time, verifying zero thermal runaway and zero signal drift under maximum rated load.
6. Preventative Maintenance Guidelines & 12-Month In-Service Warranty
To minimize future F0002 trips, plant maintenance teams should implement routine preventative maintenance checks: monitor heatsink cooling fan operation, measure DC bus filter capacitor ESR values annually, and ensure cabinet air filtration maintains ambient temperatures below 40°C (104°F).
When hardware failure does occur, Apex Industrial Control delivers fast emergency response for plant managers across Virginia, Maryland, and Washington D.C. With our 24–48 hour emergency rush turnaround service and comprehensive 12-Month In-Service Operational Warranty, your facility gets critical automation hardware restored with zero bench evaluation fee and complete operational peace of mind.